Quality Control System

Integrated Quality Assurance Across Raw Materials, Coating Lines, and Export Logistics
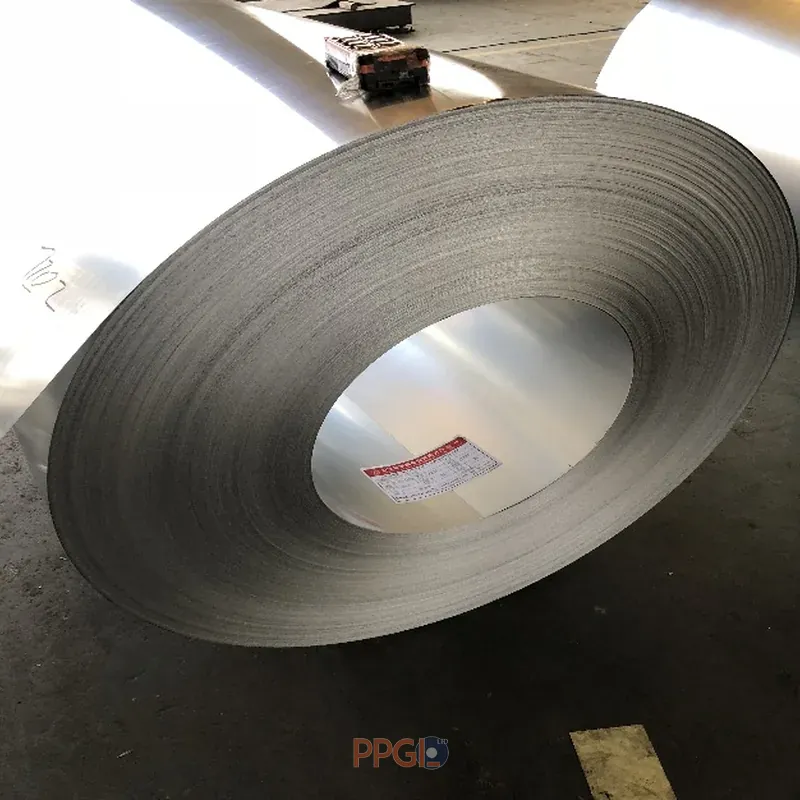
Raw material inspection before production

01 Raw Material Inspection

Substrate thickness, width, zinc mass & mechanical hardness verification before processing.

In-process color coating quality inspection line

02 In-Process Inspection

Online paint film thickness, spectrophotometer color check (ΔE), and mechanical adhesion tests.

Export seaworthy vertical packing and final inspection

03 Packing & Final Check

Inkjet coil marking validation, seaworthy waterproof packaging, and final moisture check before loading.

Raw Material Inspection
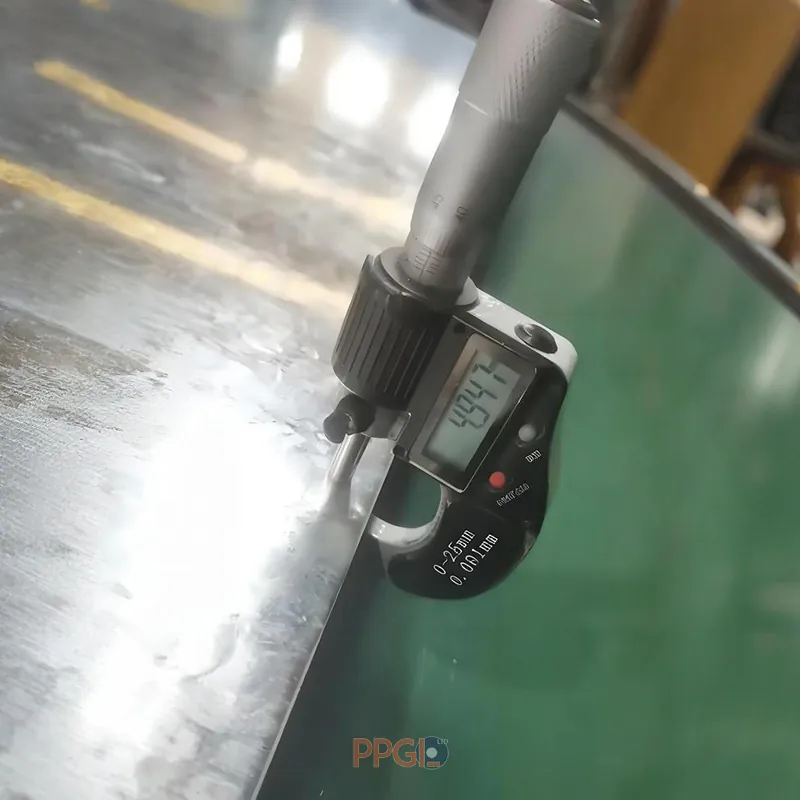
Precision micrometer testing substrate thickness and width

Thickness & Width

Precision micrometer validation of base substrate thickness and width matching order specs.

Visual inspection for surface rust or scratches on steel coil

Surface Inspection

Thorough surface check to ensure zero rust, heavy oil contamination, or mechanical scratches.

Hardness testing for steel coil substrate

Hardness Test

Hardness testing to check required substrate properties (Commercial vs. Full Hard).
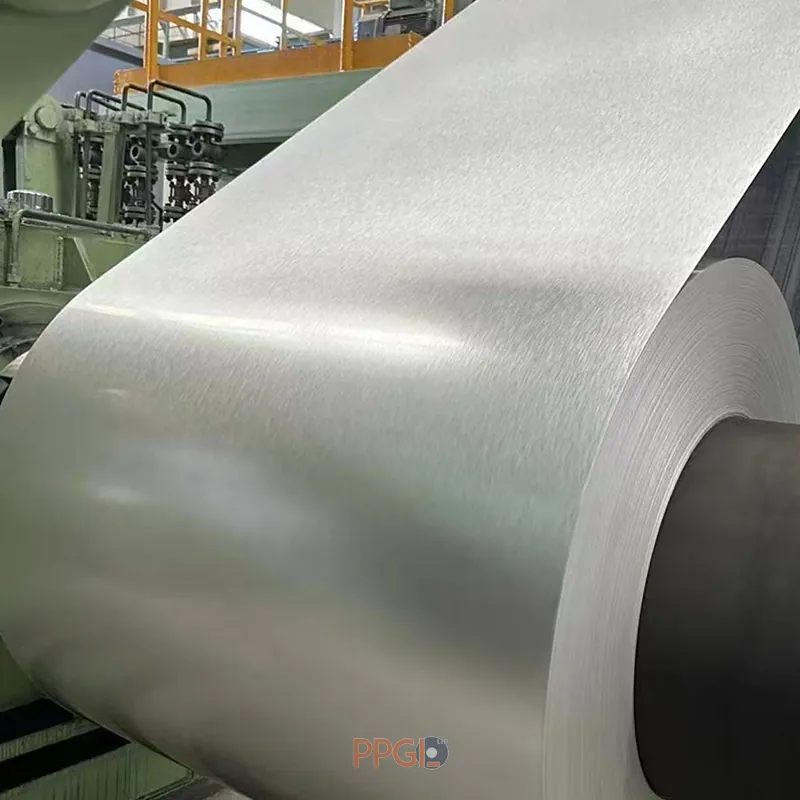
Physical coil weight check and heat number logging

Weight & Heat Number

Physical weight verification and raw material heat number matching against order specifications.

In-Process Inspection
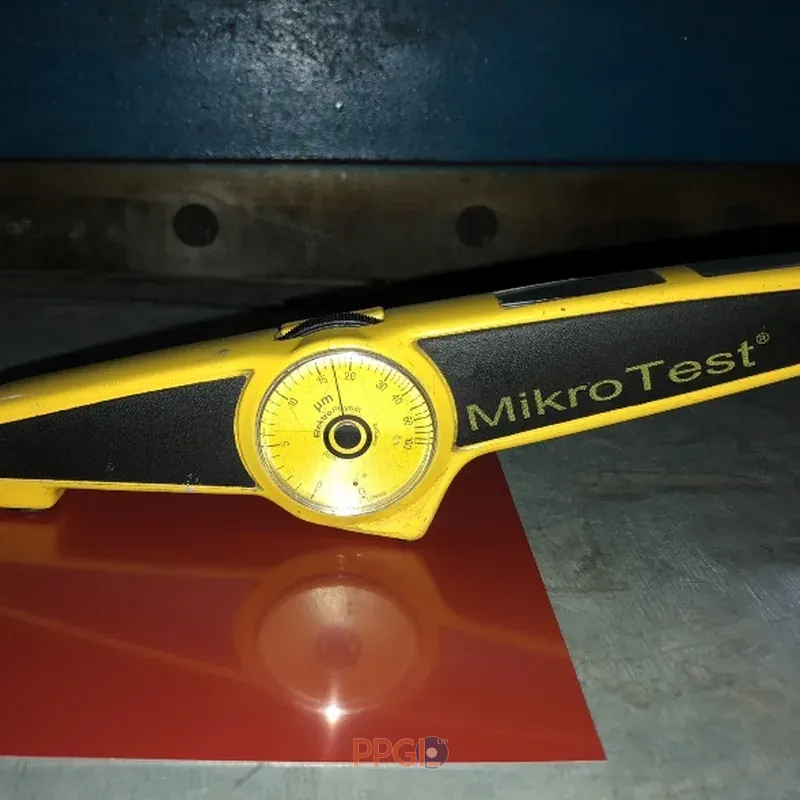
Online paint thickness measurement

Paint Thickness

Continuous online gauge testing top coat and primer thickness against target order specs.
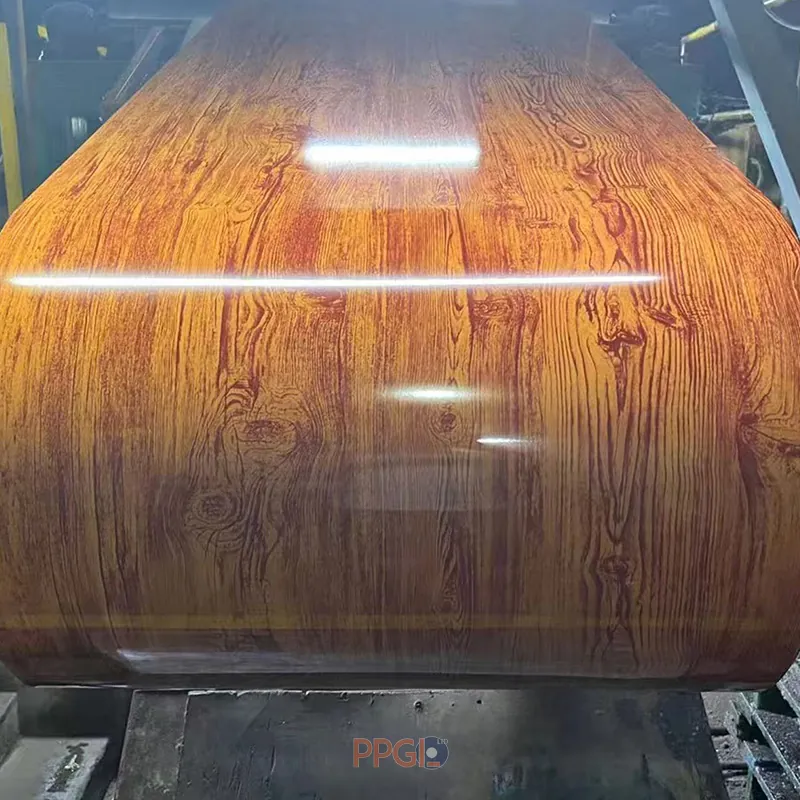
Spectrophotometer color check

Color Match

Precision spectrophotometer testing for color consistency against standard RAL codes or physical master samples.
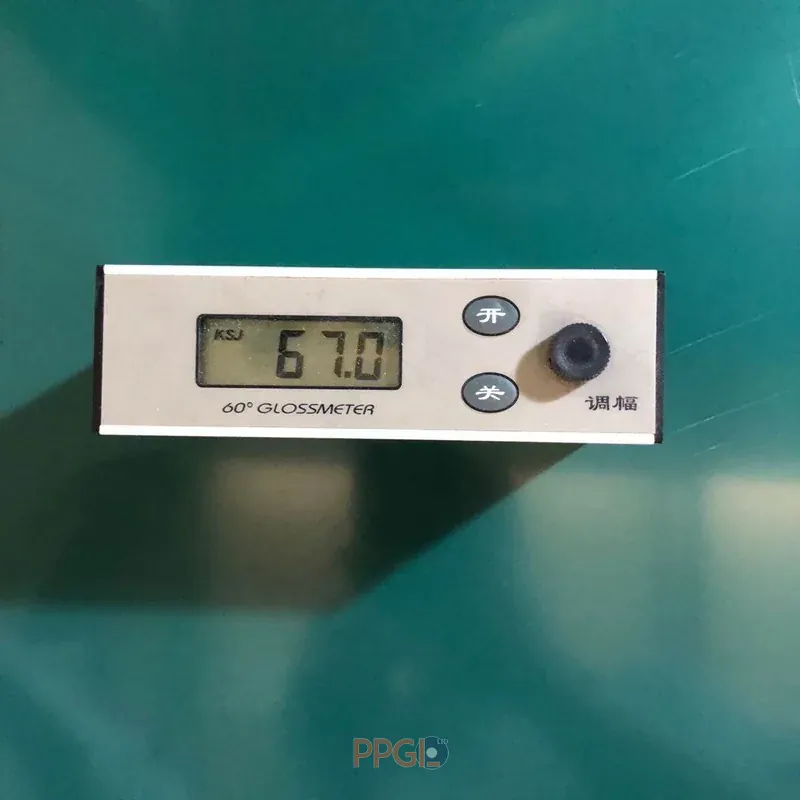
Gloss meter testing for paint surface shine

Gloss & Surface Finish

Optical gloss meter verification ensuring required surface reflection status (Matt, Semi-gloss, or High-gloss).
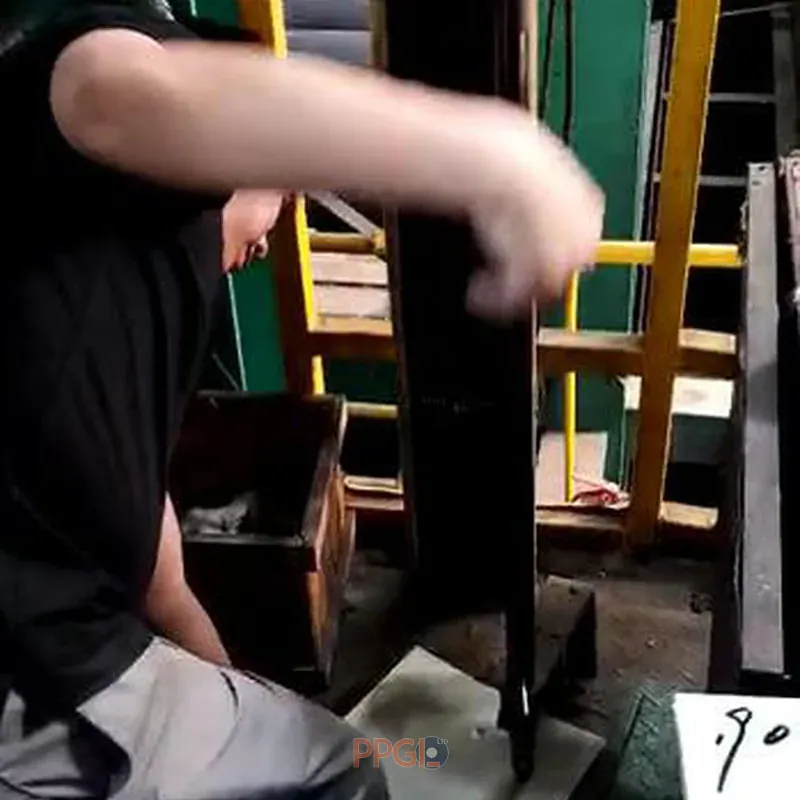
Impact resistance test for paint coating surface

Impact Test

Impact resistance testing to check paint film integrity and resistance to cracking under mechanical stress.
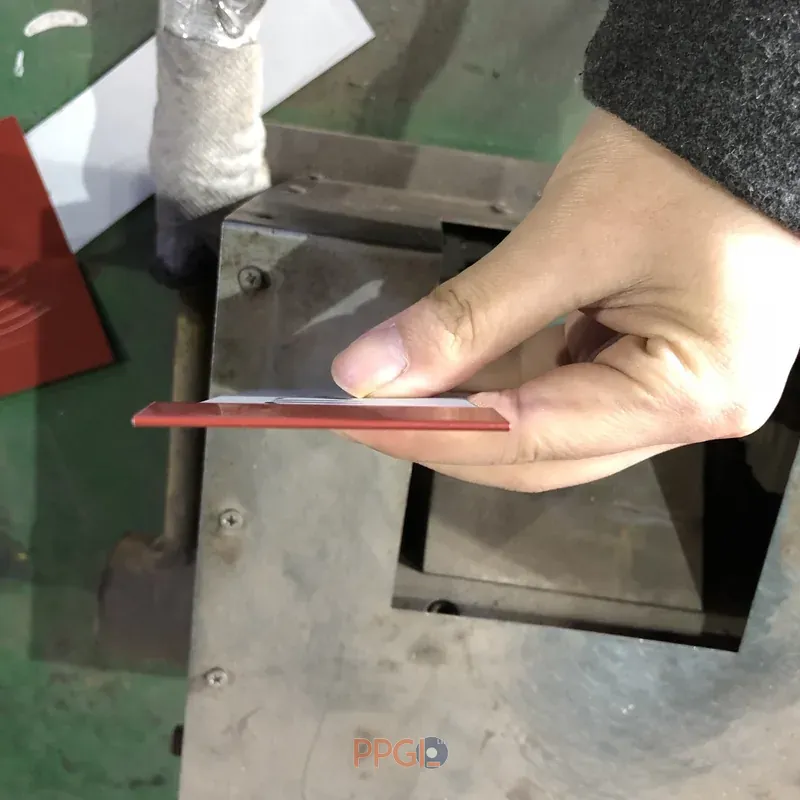
Cross hatch tape test for paint adhesion

Adhesion & T-Bend

Cross-hatch tape and T-bend testing verifying paint adhesion quality during profiling.
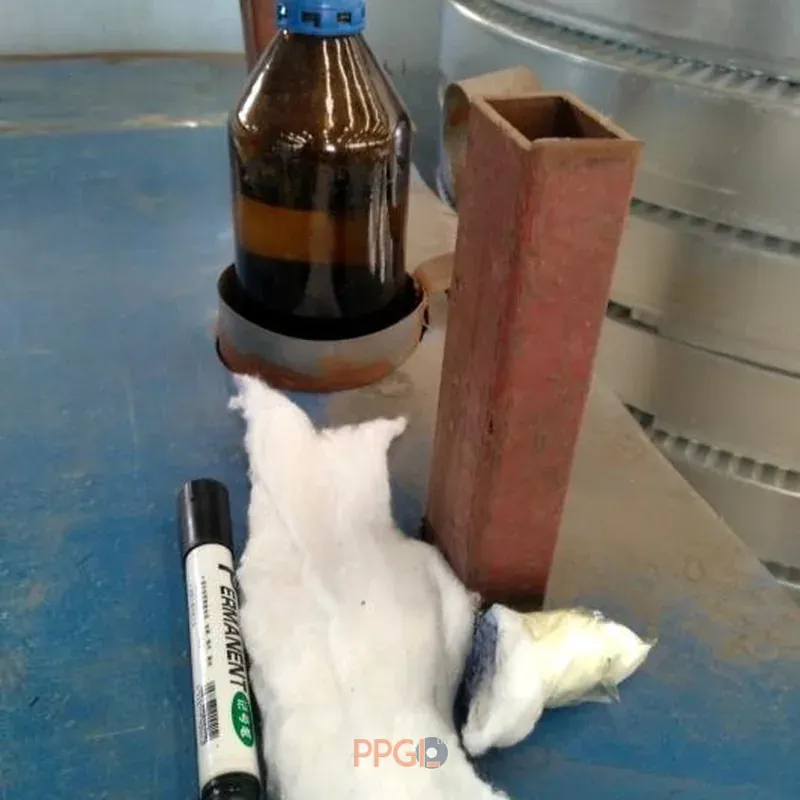
MEK rub test for paint curing quality

MEK Curing Test

Solvent double-rub testing to verify full paint film curing in the baking oven.

Packing & Final Inspection
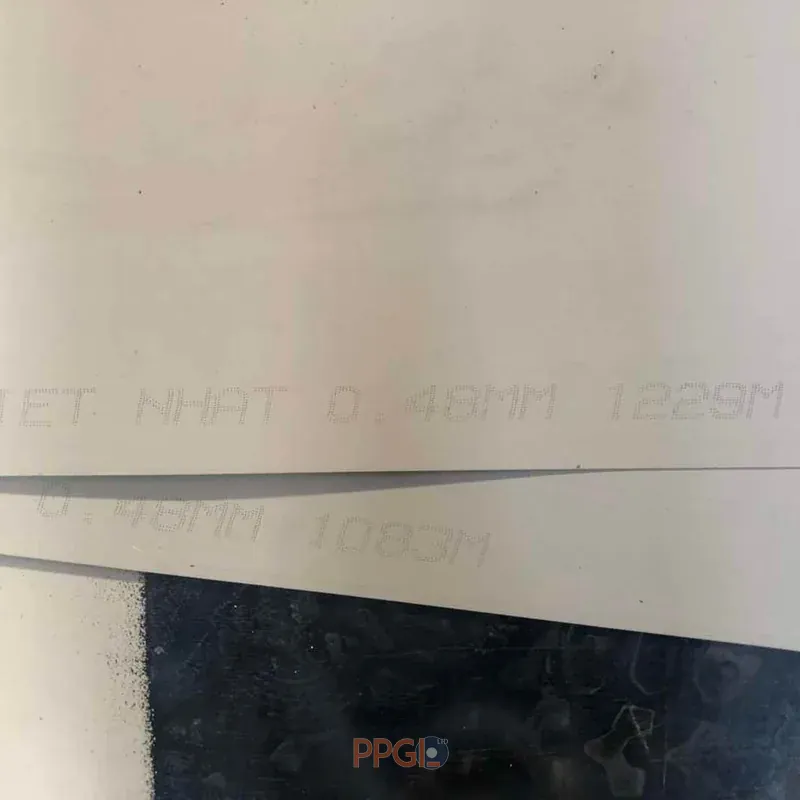
Inkjet coil marking validation on steel coil

Custom Inkjet Marking

Verification of customized inkjet marking content, brand name, and dimensions as requested by buyer.
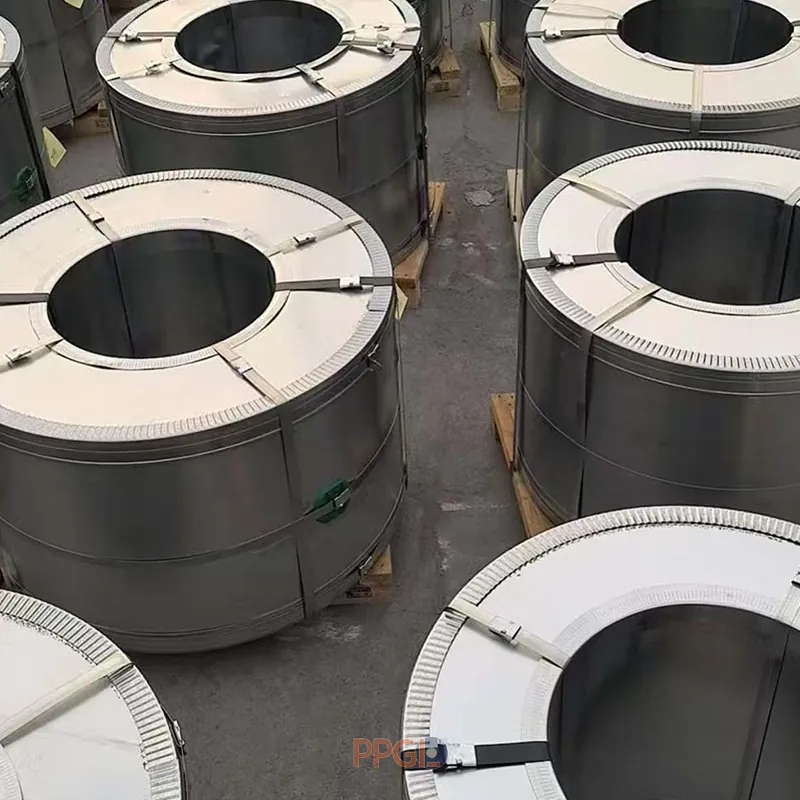
Seaworthy export packaging for steel coils

Seaworthy Packaging

Standard export packaging with anti-rust paper, plastic film, metal outer wrap, and strong steel strapping.

Weight check, label and tag inspection for export steel coils

Weight & Tag Check

Verification of gross/net coil weight, outer shipping labels, and packaging integrity prior to dispatch.

Final factory warehouse inspection prior to truck loading

Pre-Dispatch Inspection

Final visual check in factory warehouse to ensure finished coils are clean, undamaged, and ready for dispatch.

Buyer Quality Concern & FAQ

Q: How does PPGI.LTD ensure consistent quality for pre-painted steel coil exports?

A: PPGI.LTD implements a structured quality control process covering raw materials, inline production, and final export packaging. Each coil batch is monitored through continuous micrometer thickness checks, spectrophotometer color matching, paint adhesion testing (T-bend and solvent rubs), and seaworthy packaging inspection before loading.

Q: How are substrate thickness and paint coating tolerances controlled?

A: Substrate and paint film thickness are measured using precision digital micrometers and online thickness gauges. Production follows standard manufacturing tolerances (such as ASTM A755 / EN 10169) to ensure consistent dimensions along the length of each coil.

Q: How do you manage color consistency and surface gloss across production batches?

A: Color alignment is verified using digital spectrophotometers to match target RAL color codes or customer-approved physical master samples. Surface gloss levels (Matt, Semi-Gloss, or High-Gloss) are routinely checked with optical gloss meters during continuous coating runs.

Q: What inline tests are conducted to verify paint adhesion for roll forming?

A: To evaluate paint adhesion and flexibility, sample strips from each production lot undergo cross-hatch tape adhesion testing, T-bend testing, and solvent double-rub testing to confirm full paint curing prior to profiling. For detailed test requirements, feel free to contact our technical team.

error: Content is protected !!
Scroll to Top